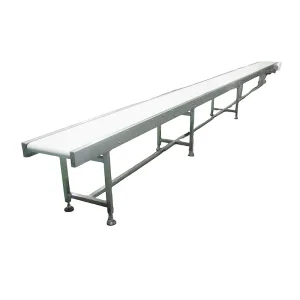
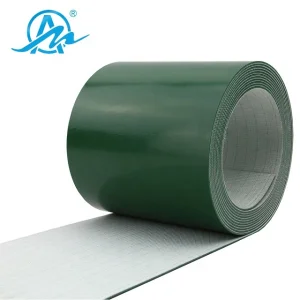
Explore our premier heavy-duty, food-grade, and customized rubber and synthetic conveying solutions deployed across modern manufacturing and processing hubs in Grenville.
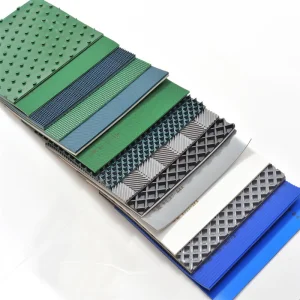
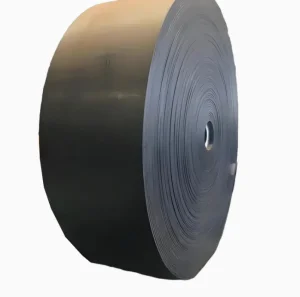
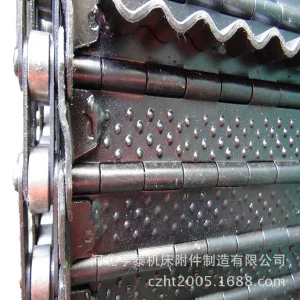
The greater Grenville region has rapidly transitioned into a pivotal nexus of advanced manufacturing, heavy industrial processing, automotive assembly ecosystems, and high-throughput e-commerce distribution networks across North America. As localized smart factories, logistics terminals, and aggregate quarry operations expand, the demand for high-reliability, friction-optimized, and wear-resistant industrial material handling belts has surged exponentially. Modern operations in Grenville can no longer afford standard, non-optimized conveying systems; unscheduled belt maintenance, tracking slippage, and material degradation directly lead to severe throughput bottlenecks and inflated Total Cost of Ownership (TCO).
Key Procurement Insight for Grenville Engineers: Elevating belt reliability requires moving beyond initial price-per-meter evaluation. Specifying tensile strength layers (EP vs NN vs Steel Cord), cover grade polymer chemistry (DIN-X vs DIN-Y vs FDA TPU), and mechanical splice integrity reduces operational energy loads by up to 18% and triples service lifespans under continuous 24/7 duty cycles.
From heavy-duty aggregate rock transport along the region’s quarries to ultra-clean food-grade processing and automated high-speed parcel sorters, industrial plants near Grenville require tailored conveyer architecture. Dongguan Trakkx Tech Co., Ltd. supplies specialized material handling belting that bridges global engineering excellence with localized operational demands, guaranteeing robust compliance with ISO 9001, CEMA (Conveyor Equipment Manufacturers Association), and FDA/USDA sanitation criteria.
Engineered material handling configurations matching the distinct mechanical stress vectors, chemical exposures, and thermal ranges of Grenville’s diverse manufacturing sector.
Designed for high impact resistance, oil/grease resilience, and severe load dispersion. Utilizing heavy steel cord reinforcement and multi-ply EP fabric (EP300-EP600) to carry stamped chassis parts, tires, and sub-assemblies without sagging or belt mis-tracking.
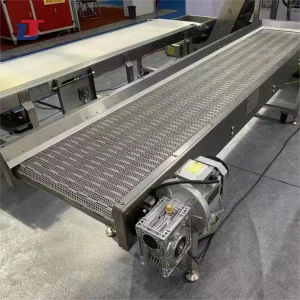
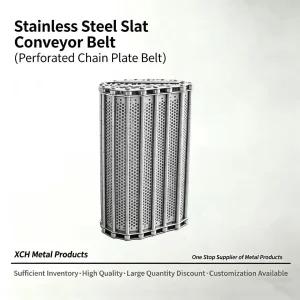
FDA-approved, EU 10/2011 compliant TPU, PU, and stainless steel mesh/plate belting. Features smooth antimicrobial coatings, hydrolytic stability, and seamless washdown tolerance to prevent bacterial harborages and streamline USDA inspections.
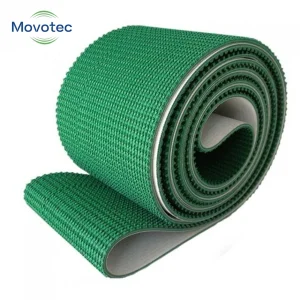
Low-noise PVC/PU synthetic belts designed for cross-belt sorters, incline cleated conveyors, and rapid fulfillment centers. Engineered with anti-static carbon filaments to eliminate electrostatic discharge in modern sensor-driven distribution hubs.
High-tensile steel cord and thick carcass rubber belting rated for extreme gouging, tearing, and high impact energy from granite, gravel, and heavy minerals. Equipped with tear-resistant breaker layers and cold-resistant compounds.
Engineering datasheet comparing key synthetic and elastomeric belt configurations available for immediate factory delivery to Grenville industrial facilities.
| Belt Polymer / Substrate Type | Tensile Rating (N/mm) | Operating Temp Range (°C) | Abrasion Resistance (mm³) | Primary Industrial Applications in Grenville |
|---|---|---|---|---|
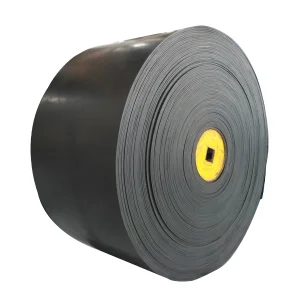
| EP Fabric Rubber (EP200 - EP600) | 200 – 3,150 N/mm | -30°C to +90°C | ≤ 120 mm³ (DIN 22102) | Mining, Aggregates, Bulk Material Handling, Scrap Metal |
| Steel Cord (ST630 - ST5400) | 630 – 5,400 N/mm | -40°C to +100°C | ≤ 90 mm³ (Heavy Wear Grade) | Long-distance Overland Conveying, Heavy Quarry Operations |
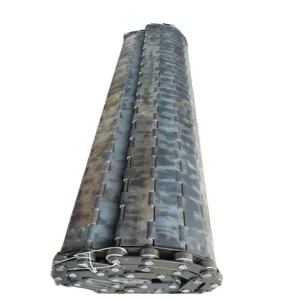
| Thermostable Stainless Steel (304 / 316L) | Rigid High Load Link Structure | -50°C to +600°C | Zero Wear / High Chemical Immunity | Industrial Baking, Dehydration, Heat Treatment, IQF Freezing |
| Thermoplastic Polyurethane (TPU) | 80 – 350 N/mm | -20°C to +80°C | High Toughness Synthetic | Food Sanitary Packaging, Pharmaceutical Conveying, Optics |
| High-Duty PVC & Cleated Belts | 100 – 400 N/mm | -15°C to +80°C | Friction Patterned / Cleated | Logistics Sorting, Incline Grain Elevators, Warehouse Automation |
Dongguan Trakkx Tech Co., Ltd. is a professional China conveyor belt manufacturer specializing in industrial material handling and conveying solutions for a wide range of industries worldwide. With years of experience in conveyor technology, we provide reliable, efficient, and customized conveyor systems that help businesses optimize production processes, improve workflow efficiency, and reduce operational costs.
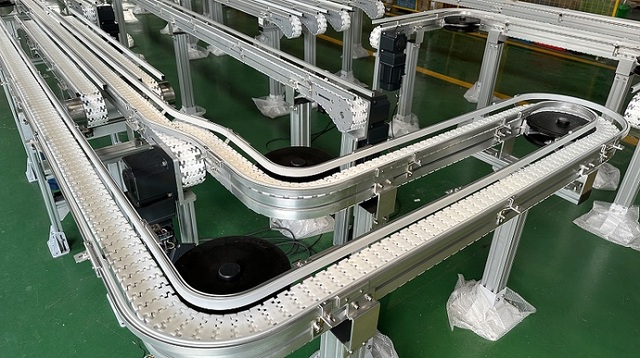
Our product portfolio includes conveyor belts, belt conveyor systems, modular conveyors, roller conveyors, inclined conveyors, assembly line conveyors, packaging conveyors, and customized material handling equipment. Designed to meet the demanding requirements of modern manufacturing environments, our solutions are widely used in logistics, food processing, electronics, automotive, warehousing, packaging, pharmaceuticals, and industrial production facilities.
At Trakkx Tech, we combine engineering expertise with advanced manufacturing capabilities to deliver high-performance conveying systems tailored to specific customer applications. Our experienced technical team works closely with clients throughout the entire process, from project consultation and system design to prototyping, production, installation support, and after-sales service.
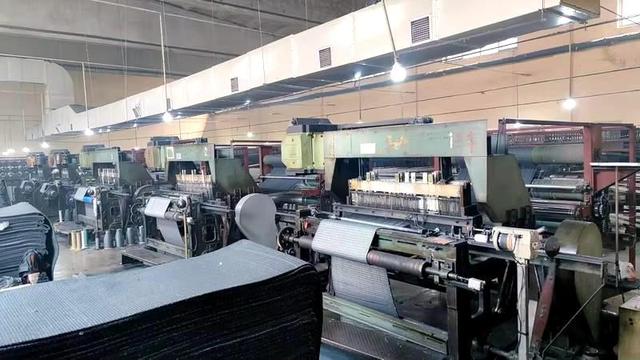
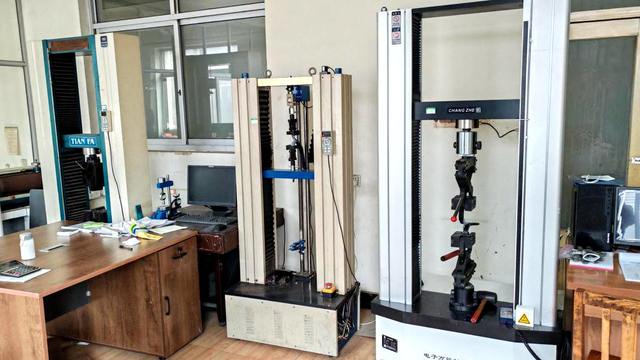
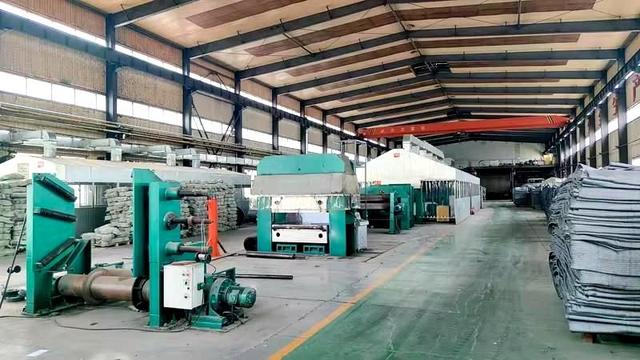
Our manufacturing facility is equipped with modern production equipment and strict quality control systems to ensure durability, reliability, and consistent performance. Every conveyor solution undergoes comprehensive testing and inspection before delivery, helping customers achieve smooth and uninterrupted material handling operations.
In addition to standard products, Dongguan Trakkx Tech Co., Ltd. offers flexible OEM and ODM services for global distributors, system integrators, equipment manufacturers, and industrial brands. We are committed to providing innovative conveying solutions that adapt to evolving industry needs and support long-term business growth.
Serving customers across North America, Europe, Southeast Asia, the Middle East, and other international markets, Trakkx Tech has established a reputation for quality, efficiency, and customer-focused service. Our mission is to become a trusted global partner for advanced conveyor belt systems and intelligent material handling solutions.
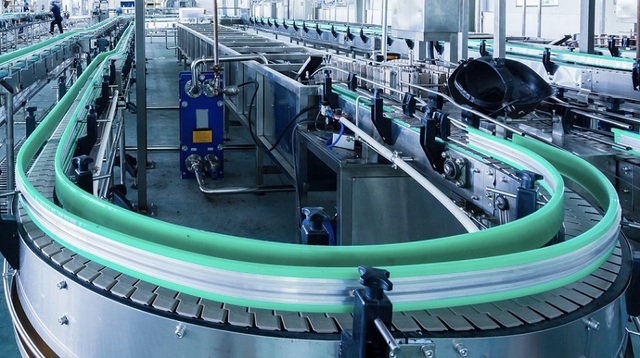
As factories across Grenville adopt IIoT architecture, industrial belts are transitioning from passive mechanical components into intelligent, data-generating operational assets.
Integration of micro RFID tags and continuous carcass thickness sensors within vulcanized rubber layers. Real-time predictive telemetry alerts plant managers in Grenville prior to delamination or mechanical rip failure, reducing unscheduled downtime to near zero.
Formulated bottom-cover elastomeric compounds that minimize indentation rolling resistance (IRR) over conveyor idlers. Reduces electrical power consumption of drive motors by up to 12-18% over long-distance bulk transfer systems.
Development of fully recyclable thermoplastic polyurethane belts containing plant-derived bio-polyols. Fully aligned with corporate ESG standards for multinational enterprise facilities operating throughout South Carolina.
In-depth technical answers regarding conveyor belt selection, maintenance optimization, splicing techniques, and localized procurement dynamics.
Browse our complete selection of standard and high-performance industrial conveyor belts. Flex-responsive layout ensures optimal alignment across all display viewports.
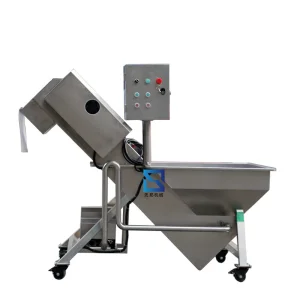
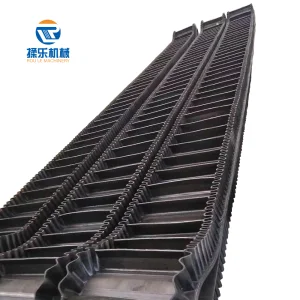
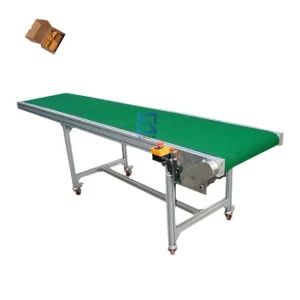
Contact Dongguan Trakkx Tech Co., Ltd. for direct factory pricing, custom engineering consultation, and rapid export delivery to Grenville manufacturing and logistics operations.
Send Inquiry Now Trakkx Tech